Sheet-metal fabrication is undergoing a practical transformation. Customers increasingly expect customized parts, smaller order quantities, rapid design changes, and dependable delivery without sacrificing dimensional consistency. For fabrication businesses, this means production equipment must support both specialization and flexibility.
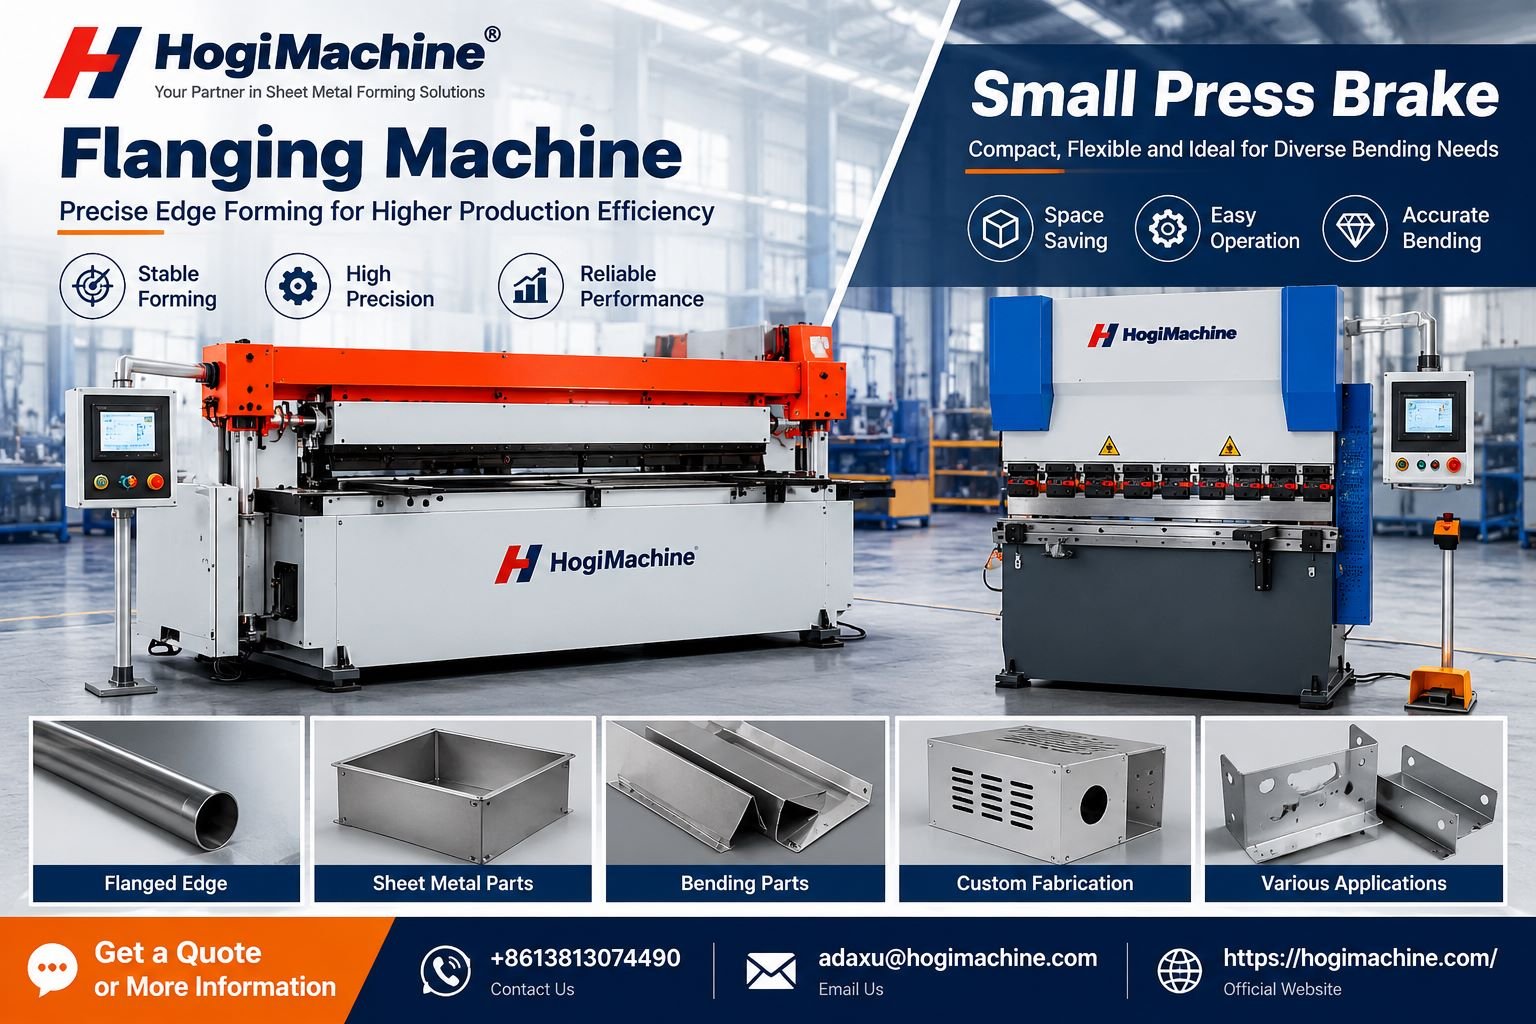
The Flanging machine is gaining importance as manufacturers seek a dedicated approach to edge forming, while the small press brake is becoming an effective option for compact bending tasks. Rather than competing for the same role, these machines can complement each other within a production environment where different components are routed according to their specific forming requirements.
Component Complexity Is Changing Machine Selection
Sheet-metal products are becoming increasingly diverse.
A single fabricated assembly may contain large panels, small mounting brackets, reinforcement pieces, covers, and components requiring formed edges.
Trying to manufacture every part using the same equipment can create scheduling bottlenecks.
Dedicated equipment provides another approach.
A Flanging machine can handle suitable edge-forming requirements while other bending work is assigned to press brake equipment. This separation allows manufacturers to organize production according to component geometry instead of forcing unrelated operations onto one workstation.
Flanging Can Improve Structural Design
A flange does more than change the appearance of a sheet-metal component.
Depending on the design, formed edges may increase stiffness, provide assembly surfaces, support joining, or help position a component within a larger product.
This makes flange design an engineering consideration.
Before production, manufacturers should examine flange dimensions, material characteristics, component geometry, and downstream requirements.
Using a Flanging machine as a dedicated production process can help workshops establish repeatable methods for components where edge geometry matters.
Small Press Brake Systems Address the “Small Part” Problem
Large press brakes are valuable assets, but they can become congested when every bending job enters the same queue.
Small components create a particular challenge.
A simple bracket may require only a few bends, yet it can occupy a larger machine that is also needed for demanding production work.
A small press brake can create a separate route for suitable compact components.
This can help manufacturers reserve larger machines for jobs that require their working length or forming capacity while giving smaller orders a dedicated production path.
Faster Response Matters for Urgent Orders
Job shops frequently receive unexpected requirements.
A customer may need replacement brackets, a revised prototype, or a small quantity of modified components on a short schedule.
If all forming equipment is occupied by larger production batches, responding quickly can become difficult.
Compact equipment can provide useful scheduling flexibility.
Where the component falls within its capabilities, a small press brake can be used for urgent bending work without significantly disrupting major jobs already assigned to larger equipment.
This can make equipment flexibility part of customer-service strategy.
Setup Standardization Can Improve Repeatability
Production consistency begins before the first component is formed.
Operators need the correct material, tooling, work instructions, and approved component information.
If these elements change between production runs, results can become less predictable.
Standardized setup sheets can help.
For repeat Flanging machine jobs, manufacturers can record relevant tooling and process information according to their internal production requirements.
Press brake jobs can similarly retain information about tooling, bend sequence, material, and inspection requirements.
The objective is to make successful manufacturing methods repeatable rather than rebuilding them every time an order returns.
Scrap Reduction Begins With Process Preparation
Material waste is a direct manufacturing cost.
A setup error that damages several components affects material, labor, machine time, and delivery schedules.
Good preparation can reduce avoidable mistakes.
Operators should confirm that they are using the correct drawing revision, material, tooling, and setup before starting a batch.
Producing and verifying an initial component can provide additional confidence before continuing with the remaining quantity.
This approach is particularly useful for custom jobs where each production batch may contain relatively few parts.
Bending Accuracy Depends on More Than the Machine
Buying accurate machinery does not automatically guarantee accurate components.
Material properties, sheet thickness, tooling, component geometry, setup, and inspection all contribute to final results.
For a small press brake, manufacturers should establish realistic component tolerances based on functional requirements and the complete forming process.
Overly restrictive tolerances can make production unnecessarily difficult, while tolerances that are too broad may cause assembly problems.
Engineering and manufacturing teams should therefore agree on requirements that support both product function and practical production.
Production Data Can Improve Quotation Accuracy
Historical manufacturing information can benefit more than the production department.
If a workshop knows how long previous setups took, which tooling was required, how many operations were performed, and what difficulties occurred, estimators can prepare future quotations with better information.
This is especially valuable for repeat orders.
Production data from Flanging machine and press brake operations can help businesses understand actual manufacturing effort rather than relying entirely on assumptions.
Better estimating can improve both pricing decisions and production planning.
Machine Footprint Is Part of Investment Planning
Factory space is a limited resource.
Manufacturers evaluating new equipment should consider not only purchase cost but also the space needed for operation, maintenance, tooling, material movement, and safety.
A small press brake may offer advantages where bending requirements are modest and available floor space is limited.
However, compact size should never replace proper capacity analysis.
The machine must still be suitable for the materials, component dimensions, and forming operations expected in daily production.
Training Creates More Flexible Production Teams
Equipment flexibility has limited value if only one employee knows how to operate a machine correctly.
Cross-training can help manufacturers develop a more adaptable workforce.
Operators should receive appropriate instruction for the equipment they use, including setup, normal operation, tooling, inspection, and relevant safety procedures.
A broader skill base can make scheduling easier when workloads change or employees are unavailable.
Training also helps ensure that documented production procedures are understood and applied consistently.
Frequently Asked Questions
What is a Flanging machine?
A Flanging machine is metal-forming equipment used to create a flange or formed edge on a workpiece for structural, assembly, joining, or other manufacturing purposes.
What does a small press brake do?
A small press brake bends appropriately sized sheet-metal components using suitable tooling and forming force.
Why use dedicated equipment for flanging?
Dedicated equipment can help standardize recurring edge-forming operations and keep other machines available for different fabrication tasks.
What parts can be produced on a compact press brake?
Depending on machine capacity, applications may include brackets, covers, panels, enclosures, prototype components, and other small fabricated parts.
Is a small press brake suitable for custom orders?
It can be well suited to custom and short-run work when the component dimensions and forming requirements fall within the machine’s rated capabilities.
How can manufacturers reduce forming scrap?
Correct drawings, verified materials, appropriate tooling, standardized setups, first-piece checks, and trained operators can help reduce avoidable errors.
Why is bend sequence important?
The order of bends can influence workpiece access, handling, tooling clearance, and the ability to complete later forming operations.
Can production records help future orders?
Yes. Historical setup, tooling, process, and inspection information can make repeat production and estimating more efficient.
What should buyers check before purchasing flanging equipment?
They should consider component geometry, flange requirements, materials, thicknesses, production quantities, machine capability, tooling, workflow, maintenance, and technical support.
How should a press brake be selected?
Selection should be based on material, thickness, bend length, required forming force, component size, tooling needs, production volume, and available factory space.
Media Contact
Sheet Metal Equipment & Project Enquiries
Contact: +86 138 1307 4490
Email: adaxu@hogimachine.com
Official Website: hogimachine.com